Small discrepancies between datasheet dimensions and PCB land patterns are a leading cause of assembly defects; this guide breaks down the GMT10X7R153K50NT4 datasheet into the exact inputs you need to design a reliable footprint. This introduction uses the part name once and calls out both footprint and datasheet so designers focus immediately on dimension extraction, conversion, and verification before CAD implementation. The goal: reduce first-pass failures by translating mechanical tolerances into concrete pad and paste rules.
1 — Background: What GMT10X7R153K50NT4 is and which datasheet fields matter
1.1 Part ID decode & component class
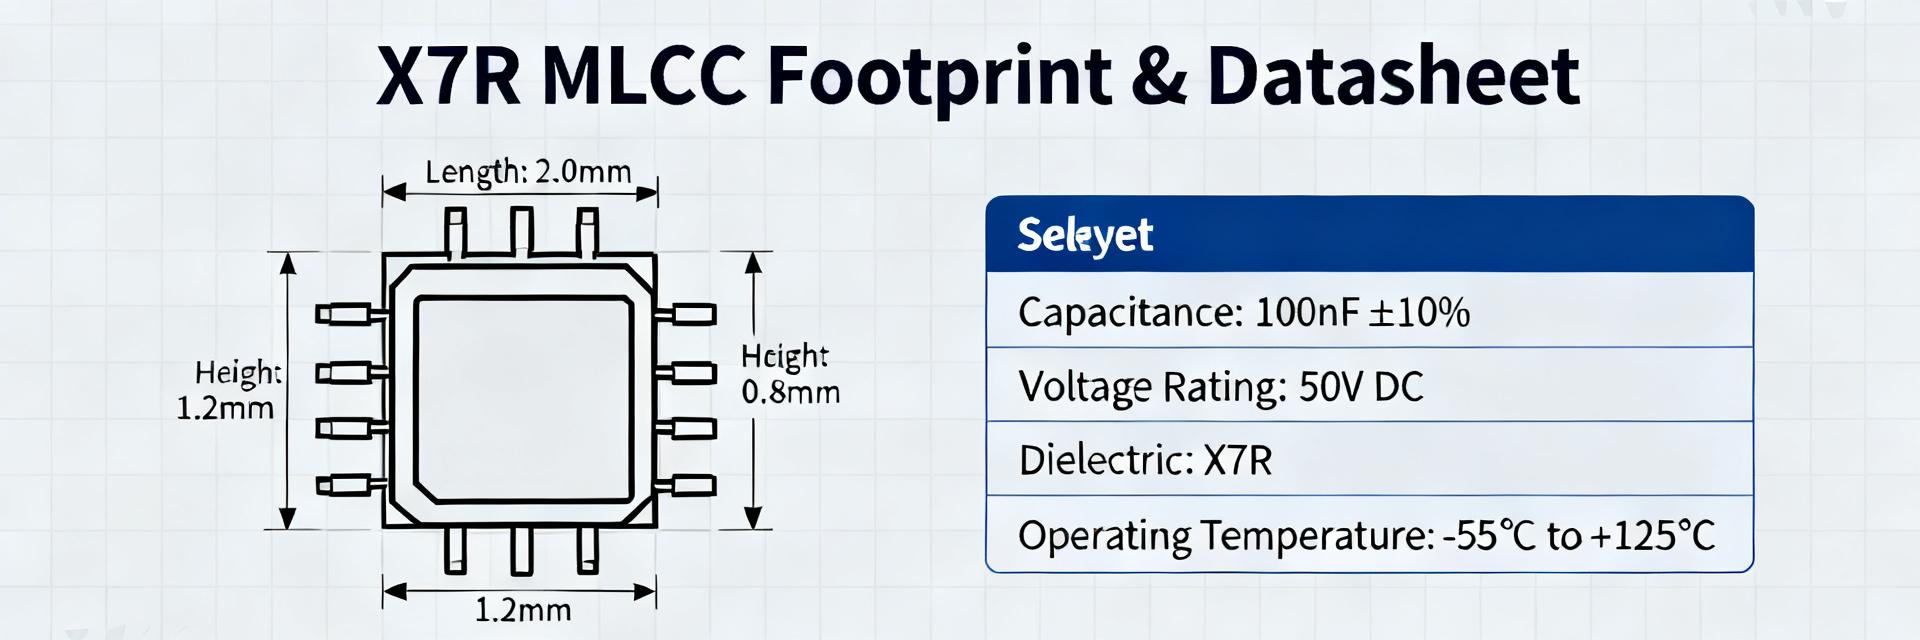
Point: Read the part ID to extract dielectric, nominal capacitance, tolerance, rated voltage, and packaging code. Evidence: Standard capacitor nomenclature embeds X7R dielectric, 15nF nominal value, K tolerance, and a voltage code. Explanation: This indicates an MLCC-style ceramic capacitor where mechanical and electrical specs both influence footprint choice; both termination geometry and coplanarity matter for solder fillet and reliability.
1.2 Typical datasheet sources & version control
Point: Use the authoritative datasheet revision and confirm units and drawings. Evidence: Datasheets include a revision/date and sectional drawings; inconsistent unit usage (mm vs mil) causes footprint errors. Explanation: Maintain a checklist: drawing revision, measurement units, tolerance notes, and recommended land pattern table, and record the datasheet revision in your PCB library entry for traceability.
2 — Datasheet deep-dive for GMT10X7R153K50NT4 (mechanical & electrical inputs)
2.1 Mechanical dimensions to extract (body, terminations, tolerances)
Point: Capture overall length/width/height, termination length/width, coplanarity, recommended land pattern, and dimensional tolerances. Evidence: 2D drawings and section views list min/typ/max for each dimension. Explanation: Convert min/typ/max into footprint constraints and clearance envelopes—use max body to set courtyard, min termination to set minimum copper exposure, and coplanarity to set acceptable placement tolerance.
2.2 Electrical / assembly limits that affect footprint choice
Point: Electrical specs like rated voltage, dielectric (X7R), and temperature coefficient affect assembly choices. Evidence: X7R dielectrics are mechanically sensitive under thermal cycling; rated soldering temperatures and max reflow profiles appear in the datasheet. Explanation: Use the reflow temperature and allowable soldering time to set paste profile and assembly process; note any cleaning or handling constraints that change pad/mask choices.
3 — Designing the footprint for GMT10X7R153K50NT4: pad geometry, paste, and mask
3.1 Pad geometry & dimensioning (formulaic approach)
Point: Derive pad dimensions from termination and body measurements using margin rules. Evidence: Best practice uses termination exposure on copper = termination length minus a small overlap and IPC baselines as starting points. Explanation: Formulaic steps: pad length = termination length + overlap allowance; pad width = termination width + X mm (manufacturing margin); pad spacing = body length + tolerance clearance. Include sample placeholders for data-driven calculations in the table below.
| Parameter | Datasheet Value (fill) | Calculation |
|---|---|---|
| Body length (L) | [L_min / L_typ / L_max] | Courtyard = L_max + 0.5 mm |
| Termination length (tL) | [tL_min / tL_typ / tL_max] | Pad length = tL_typ + 0.15 mm |
| Termination width (tW) | [tW_min / tW_typ] | Pad width = tW_typ + 0.10 mm |
3.2 Paste mask, solder fillet, and thermal considerations
Point: Size paste apertures to control solder volume and fillet formation; consider thermal mass. Evidence: Datasheet reflow guidance and termination geometry dictate paste percent and whether split apertures are required. Explanation: Use 60–80% paste coverage for single apertures, split the aperture for long terminations, and avoid large adjacent pours that create thermal sinks—use pour islands or thermal spokes to reduce warpage.
4 — CAD implementation, 3D model and verification
4.1 Creating/validating the footprint in your CAD tool
Point: Implement pad outlines, mask openings, courtyard, and reference designators per extracted values. Evidence: DRC rules validate pad-to-pad spacing, solder paste coverage, and annular mask constraints. Explanation: Set layer attributes, assign pin numbers consistently, and run a DRC checklist: pad spacing, paste coverage percentage, mask-to-pad annular clearances, and courtyard clearance relative to maximum body dimension.
4.2 3D model, mechanical checks and prototype validation
Point: Build or import a 3D STEP model from datasheet dimensions and verify clearances. Evidence: 3D clearance checks reduce assembly rework by highlighting silkscreen or component interference. Explanation: Prototype flow: print a single-board panel, place components, inspect fillets and coplanarity with X-ray or optical microscopy, and record deviations back into the footprint library for revision control.
5 — Troubleshooting common footprint/datasheet mismatches & pre-production checklist
5.1 Common mismatch scenarios and fixes
Point: Frequent issues include unit mismatches, using vendor pad defaults, paste overrun, and incorrect courtyard. Evidence: Errors stem from copying vendor footprints without cross-checking datasheet min/max and recommended land patterns. Explanation: Fixes: always convert units, prefer datasheet land pattern over vendor defaults unless validated, adjust paste percent to prevent overrun, and set courtyard to max body plus margin.
5.2 Final pre-production checklist for GMT10X7R153K50NT4
Point: Run a compact checklist before generating Gerbers. Evidence: A short checklist reduces first-article failures and speeds design-signoff. Explanation: Checklist: note datasheet revision, match footprint dims to drawings, verify paste openings, check 3D clearances, pass prototype inspection, and log library version and verifier name in the BOM entry (include datasheet revision and footprint filename).
Summary
Accurate extraction of mechanical specs from the GMT10X7R153K50NT4 datasheet, formulaic pad derivation, CAD verification, and a concise prototype check are the fastest route to reliable assemblies. The datasheet must drive pad geometry, paste percent, and thermal decisions; the footprint and CAD model should be versioned with the datasheet revision and validated with a prototype run to capture real-world coplanarity and fillet behavior.
Key Summary
- Extracted mechanical dimensions (body, terminations, coplanarity) from the datasheet set pad and courtyard limits; always use max body for courtyard sizing and record the datasheet revision.
- Derive pad length and width from termination typ values plus small manufacturing margins; use IPC baselines and document calculation placeholders in the footprint library.
- Set paste aperture to ~60–80% (split if needed), align reflow profile to datasheet thermal limits, and validate with a short prototype build—log deviations into library version control.
Common Questions
How do I ensure the GMT10X7R153K50NT4 footprint matches the datasheet?
Compare each pad and courtyard dimension directly to the datasheet min/typ/max values, convert units carefully, and create calculation notes in the footprint metadata. Validate with a 3D STEP model and a prototype placement to inspect fillet shape and coplanarity. Record the datasheet revision and verifier name in the BOM entry to maintain traceability.
What paste mask rules work best for ceramic capacitors like GMT10X7R153K50NT4?
Start with 60–80% paste coverage for a single aperture; if long terminations risk excess solder, split the aperture along the pad length to control volume. Tailor paste percentage based on prototype fillet observations and adjust stencil thickness or stepdown for fine tuning. Always reference the reflow limits in the datasheet when setting thermal process parameters.
Which CAD checks catch the most footprint errors before fabrication?
Run DRC for pad-to-pad spacing, solder paste coverage, annular mask clearance, and courtyard clearances set from max body dimensions. Add a 3D clearance check for silkscreen and nearby components, and include the datasheet revision and calculation notes in the footprint properties so reviewers can confirm assumptions during sign-off.
How does the X7R dielectric and thermal limits impact PCB assembly?
X7R dielectrics are mechanically sensitive under thermal cycling. PCB designers must align the paste profile and stencil dwell to the datasheet's rated reflow limits, and isolate the component from large adjacent thermal masses using thermal spokes to prevent mechanical cracking.